The Scale of the Challenge
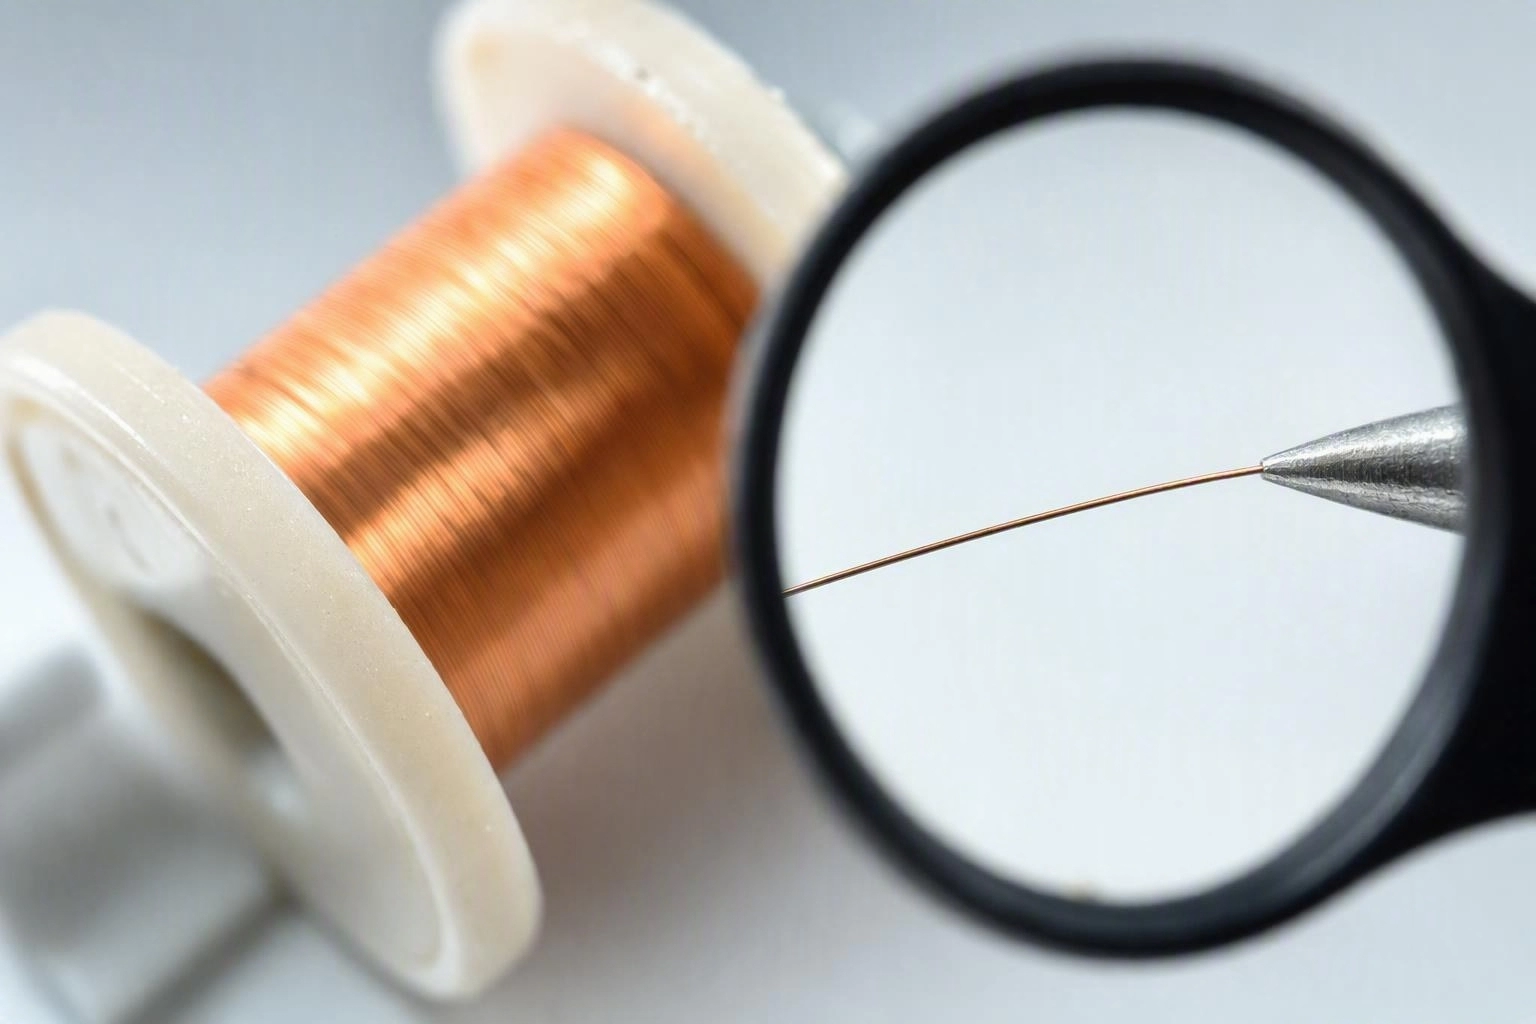
At 0.03 mm, an enameled copper conductor is thinner than a human hair. The insulation layer on such a wire may be only a few micrometres thick, and yet it must withstand the winding tension, the bending radius of a small coil and the voltage applied to the circuit. A defect that would be irrelevant on a 2 mm wire — a single pinhole, a thin patch, a particle inclusion — is a functional failure at this scale.
Ultra-fine wire is therefore less a product of scale than a product of process control. The manufacturers who can supply it reliably are those who have mastered consistency across drawing, coating, curing and inspection.
Where Ultra-Fine Wire Is Used
- Miniature sensors and transducers — pickups, microphones and precision measurement coils.
- Medical devices — implantable and diagnostic equipment where size and reliability are both critical.
- Consumer electronics — earbuds, haptic actuators, small vibration motors.
- Instrumentation and metering — precision coils where stability matters more than power.
- Aerospace and defence — compact high-reliability windings.
The Manufacturing Sequence
Wire drawing
Rod is drawn down through a series of dies to the final diameter. At ultra-fine gauges, the final passes involve very small reductions per die and require precise lubrication and die condition control. Any surface damage introduced at this stage is carried forward and cannot be coated over reliably.
Annealing
Drawn copper must be annealed to restore the softness needed for winding. At fine gauges, annealing is often performed continuously in line with drawing to avoid handling damage and oxidation between steps.
Enamel application
Multiple thin coats are applied rather than a single thick coat, because each coat must cure completely before the next is applied. Coating thickness is controlled by dies or felts, and the concentricity of the coating around the conductor is as important as its average thickness. Eccentric coating leaves one side of the wire electrically weak even when the nominal build specification is met.
Curing
Each enamel layer is cured in an oven. Temperature profile determines the degree of cure, which in turn governs flexibility, adhesion and dielectric strength. Under-cured enamel is soft and prone to damage; over-cured enamel is brittle. At ultra-fine gauges, the wire passes through the oven quickly and the thermal profile must be tightly controlled.
Inspection and spooling
Final inspection includes diameter measurement, pinhole detection and continuity testing. Spooling tension must be controlled to avoid stretching or surface damage, and spool geometry must suit the customer's winding equipment at very fine gauges where tension sensitivity is high.
Quality Measurements That Matter
| Parameter | Why it matters at fine gauge |
|---|---|
| Conductor diameter | Directly sets resistance; small errors have large relative effect |
| Overall diameter | Determines whether the wire fits the intended coil geometry |
| Coating concentricity | Eccentricity creates a thin side that fails under voltage stress |
| Pinhole count | Primary indicator of coating continuity across the length |
| Elongation | Predicts whether the wire survives winding without cracking |
| Adhesion after elongation | Confirms the coating stays attached when the wire is deformed |
| Dielectric breakdown | Confirms insulation capability in the finished state |
| Solderability | Critical for grades intended to be terminated without stripping |
Handling Ultra-Fine Wire in Production
Even perfect wire can be ruined by poor handling. Users of ultra-fine wire should consider:
- Controlling unwinding tension precisely, because fine wire deforms permanently under modest over-tension.
- Minimising guide and roller contact points, each of which is an opportunity for abrasion.
- Avoiding sharp radii, since bending stress concentrates at the outside of the bend.
- Keeping the working area clean, because airborne particles can damage fine coatings.
- Storing spools in controlled conditions to limit moisture and temperature variation.
Specifying Ultra-Fine Wire
- State the conductor diameter and the required overall diameter, not just a build grade code.
- Specify whether solderability is required and after what ageing exposure.
- Define the acceptable pinhole level for the length used in production.
- Confirm the thermal class if the coil operates warm, since fine wire has less thermal mass.
- Ask for a sample for winding trials, as fine wire behaviour depends heavily on the machine.
Manufacturing Range
Huaya Fa produces enameled round wire from 0.03 mm upwards, covering polyurethane, polyester and polyester-imide insulation systems across class 130 to class 200, in copper and in self-bonding variants. Production is supported by ISO 9001 and ISO 14001 certification, and material compliance documentation for RoHS and REACH is available per shipment.
For ultra-fine gauges we recommend an early winding trial with production-representative samples, because the interaction between wire, tension and coil geometry is where most fine wire problems actually originate.